

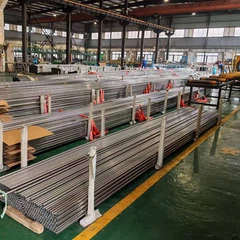
ASTM A312 TP316L Seamless Stainless Steel Pipe for Petrochemical Service
Sep 28, 2025
Leave a message
ASTM A312 TP316L is a low carbon austenitic stainless steel seamless pipe built for corrosive, high temperature and high pressure service. In the designation, TP stands for tubular product, 316 identifies the molybdenum bearing chromium nickel family, and the letter L marks the low carbon version. Because carbon is limited to 0.03 percent maximum, the pipe resists sensitisation and intergranular corrosion after welding, which makes it a common choice for chloride bearing process streams in chemical, petrochemical, textile and food plants.
What Is ASTM A312 TP316L?
ASTM A312 and its ASME equivalent SA312 cover seamless, straight seam welded and heavily cold worked austenitic stainless steel pipe intended for high temperature and general corrosive service. The seamless route starts from a pierced billet that is hot rolled or cold drawn to the finished size, so the pipe has no longitudinal weld and no filler metal in the wall.
TP316L is fully austenitic at ambient temperature and cannot be hardened by heat treatment. It is supplied in the solution annealed condition, is essentially non magnetic when annealed, and keeps useful toughness from cryogenic service temperatures up to the elevated range where oxidation resistance and phase stability, rather than creep strength, become the limiting factors.
Chemical Composition of ASTM A312 TP316L
| Element | Requirement, % | Function |
|---|---|---|
| Carbon | 0.03 max | Held low to avoid carbide precipitation at grain boundaries |
| Manganese | 2.00 max | Deoxidation and austenite stability |
| Phosphorus | 0.045 max | Residual element, held low for weldability |
| Sulfur | 0.030 max | Residual element, held low for hot workability |
| Silicon | 0.75 max | Deoxidation |
| Chromium | 16.0 - 18.0 | Passive oxide film and oxidation resistance |
| Nickel | 10.0 - 14.0 | Stabilises the austenitic structure and improves toughness |
| Molybdenum | 2.00 - 3.00 | Resistance to pitting and crevice corrosion in chloride service |
| Nitrogen | 0.10 max | Interstitial strengthening within the specification limit |
Mechanical Properties in the Annealed Condition
| Property | Minimum value |
|---|---|
| Tensile strength | 485 MPa |
| Yield strength, 0.2 percent offset | 170 MPa |
| Elongation in 50 mm | 40 percent |
| Hardness | 217 HB maximum |
Size Range, Schedules and End Finish
Nominal bore from 1/8 inch NB to 24 inch NB
Outside diameter from 6.00 mm to 914.4 mm
Wall thickness from 0.3 mm to 50 mm
Schedules: SCH 5, SCH 10, SCH 20, SCH 30, SCH 40, STD, SCH 60, SCH 80, SCH 80S, XS, SCH 100, SCH 120, SCH 140, SCH 160 and SCH XXS
Manufacturing routes: seamless hot rolled and seamless cold drawn, hot finished or cold finished
Lengths: single random, double random and specified cut length
Ends: plain end, beveled end and threaded end
Forms: round, square, rectangular and hydraulic tube
Heat Treatment and Fabrication
Solution annealing is carried out between 1010 °C and 1120 °C followed by rapid cooling in water or air. The treatment dissolves chromium carbides, removes cold work strain and restores corrosion resistance, so slow cooling through the sensitisation range must be avoided. Because the grade does not respond to hardening by heat treatment, higher strength can only be obtained by cold work, which is why hydraulic and instrument tube is often supplied in a cold drawn temper.
The pipe is readily welded by GTAW, GMAW and SMAW processes with a matching low carbon filler, bent cold or hot, and machined with standard austenitic practice. Weld areas are cleaned and passivated after fabrication to remove heat tint and rebuild the passive film.
Typical Applications
Chemical processing equipment and reaction vessels
Petroleum refining and petrochemical process piping
Food processing and pharmaceutical hygienic lines
Pulp and paper mill liquor and bleaching lines
Marine exteriors, desalination and other chloride bearing services
Textile dyeing equipment and heat exchanger tubing
Quality Control, Marking and Delivery
Each heat is verified by chemical analysis and each lot by tensile testing, and the pipe is submitted either to a hydrostatic test or to an electric non destructive examination before despatch. Products are marked with the standard, grade, size, heat number and method of manufacture, and are supplied with test certificates covering chemical composition, mechanical properties and dimensional inspection. Cold drawn and annealed pipe is delivered with protective caps and sealed ends so that the bore stays clean during transport.
Frequently Asked Questions
Q: What does the L in TP316L mean?
The letter L marks the low carbon version of the 316 chemistry, with carbon held to 0.03 percent maximum so that welded joints resist intergranular corrosion.
Q: Is ASTM A312 TP316L pipe seamless or welded?
A312 covers both types; the pipe described here is seamless, produced by hot rolling or cold drawing from a pierced billet with no longitudinal weld.
Q: What is the difference between 316 and 316L pipe?
Both contain 16.0 to 18.0 percent chromium, 10.0 to 14.0 percent nickel and 2.00 to 3.00 percent molybdenum; 316 allows 0.08 percent carbon while 316L allows 0.03 percent, which improves weld zone corrosion resistance at a small cost in annealed strength.
Q: Which schedules and sizes are available?
Nominal bore from 1/8 inch to 24 inch, outside diameter from 6.00 mm to 914.4 mm, and schedules from SCH 5 through SCH 160 and XXS.
Q: How is the pipe heat treated?
It is solution annealed at 1010 °C to 1120 °C and cooled rapidly; the grade cannot be strengthened by quenching or tempering.
Q: Should TP316L be used in the sensitisation temperature range?
Continuous service in the range of roughly 425 °C to 815 °C should be assessed carefully, because chromium carbide precipitation can reduce corrosion resistance even in the low carbon grade.
Q: What end finishes are supplied?
Plain end, beveled end and threaded end, in single random, double random or specified cut lengths.
Send Inquiry