

X8CrNiS18-9 (1.4305) AISI 303 Free-Cutting Stainless Steel: Properties and Applications
Jun 04, 2025
Leave a message
What Is X8CrNiS18-9 (1.4305) Stainless Steel?
X8CrNiS18-9 is the EN designation of the free-cutting austenitic stainless steel known commercially as AISI 303, with EN material number 1.4305 and UNS number S30300. The grade sits in the 18% chromium / 9% nickel austenitic family, but a deliberate sulfur addition makes it machine considerably faster than standard 304. Chips break cleanly, cutting forces fall and surface finish is easier to hold, which is why turned parts such as fasteners, shafts, bushings and precision fittings are so often produced from this steel.
The trade-off is a modest reduction in corrosion resistance, because manganese sulfide inclusions interrupt the passive chromium oxide film. Designers therefore specify X8CrNiS18-9 where the service environment is only mildly corrosive and where machining cost dominates total part cost. The grade remains austenitic at room temperature, keeps good toughness and shows the familiar non-magnetic response of the 300 series in the annealed condition.
Chemical Composition of X8CrNiS18-9 (1.4305)
The cast analysis limits below follow EN 10088-2. Elements that are not listed are not intentionally added without agreement between supplier and purchaser.
| Element | C | Si | Mn | P | S | Cr | Ni | N | Cu |
|---|---|---|---|---|---|---|---|---|---|
| Mass fraction, % | max 0.10 | max 1.00 | max 2.00 | max 0.045 | 0.15-0.35 | 17.0-19.0 | 8.0-10.0 | max 0.11 | max 1.00 |
Sulfur between 0.15% and 0.35% forms manganese sulfide stringers that act as internal chip breakers along the cutting shear plane. Chromium at 17-19% builds the passive layer, while nickel at 8-10% stabilises the austenitic structure so that ductility stays workable.
Mechanical and Physical Properties
| Property | Typical value |
|---|---|
| Tensile strength | 500-750 MPa |
| 0.2% proof strength | min 190 MPa |
| Elongation | min 35% |
| Hardness | max 230 HB |
| Density | 7.9 g/cm3 |
| Modulus of elasticity | approx. 193 GPa |
| Structure | Austenitic |
| Magnetic behaviour | Non-magnetic annealed; slightly magnetic after cold work |
These values refer to the annealed condition. Cold drawing raises strength and hardness while reducing elongation, so finished parts should always be assessed in the condition actually delivered.
Equivalent Grades and Cross-Reference
| Standard system | Grade |
|---|---|
| EN | X8CrNiS18-9 (1.4305) |
| AISI / SAE | 303 |
| UNS | S30300 |
| JIS | SUS 303 |
| ISO | X8CrNiS18-9 |
| GB (China) | Y1Cr18Ni9 free-cutting grade |
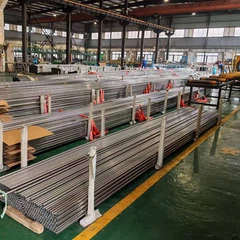
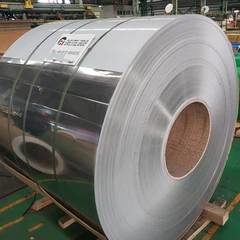
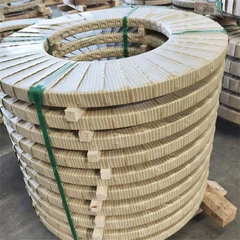
Product forms are covered by EN 10088-1, EN 10088-2, EN 10088-3, EN 10088-5 and EN 10297-2, which together define composition, properties and delivery conditions for plate, strip, bar, rod, wire, sections and seamless tube.
Machinability, Welding and Corrosion Behaviour
Machinability: the highest of the common austenitic grades, well suited to high-speed turning, threading and automatic screw machines.
Welding: not recommended, because the sulfur addition raises hot-cracking risk in the fusion zone. Where a joint is unavoidable, filler metal and heat input must be controlled and the design reviewed.
Corrosion: resistance is lower than that of 1.4301 (304). Chloride-bearing, marine and strongly acidic environments promote pitting and crevice attack at the sulfide inclusions.
Magnetism: non-magnetic in the annealed state, slightly magnetic after cold working.
Alternatives: when corrosion resistance matters more than machining speed, specify 1.4301 (304) or 1.4404 (316L).
Typical Applications
Fasteners: hex bolts, nuts, screws, studs and threaded rod
Turned and ground shafts, spindles and valve stems
Bushings, sleeves and small precision fittings
Pump and instrument components with limited chloride exposure
Automatic screw-machine parts and general industrial hardware
Selection should be confirmed against the actual medium, temperature and required service life rather than by grade familiarity alone.
Frequently Asked Questions
Q: Can X8CrNiS18-9 (1.4305) be welded?
Welding is not recommended because the sulfur addition raises the risk of hot cracking in the weld pool. If a joint is essential, heat input and filler metal must be controlled.
Q: Is 1.4305 magnetic?
It is non-magnetic in the annealed condition, but may become slightly magnetic after cold working such as drawing, bending or thread rolling.
Q: What is the difference between 1.4305 and 1.4301?
Both are austenitic 18/8-type steels. 1.4305 carries a deliberate sulfur addition for free-cutting behaviour and machines much faster, while 1.4301 (304) contains no deliberate sulfur and resists corrosion better.
Q: What is the maximum hardness of 303 stainless steel?
The specification limit is 230 HB maximum in the annealed condition.
Q: Which grade replaces 303 when corrosion resistance is the priority?
1.4301 (304) for general service and 1.4404 (316L) for chloride-bearing or more aggressive media, accepting slower machining.
Q: Which standards cover X8CrNiS18-9?
EN 10088-1, EN 10088-2, EN 10088-3, EN 10088-5 and EN 10297-2 define composition, properties and delivery conditions for the relevant product forms.
Send Inquiry