

304 and 316 Stainless Steel Profiles for Photovoltaic Mounting Systems
Aug 12, 2025
Leave a message
Why Solar Mounting Systems Are Built from Stainless Profiles
A photovoltaic array is designed for a service life measured in decades, and the structure underneath it has to survive every one of those years without a repaint. Hot-dip galvanising performs well inland, but in coastal air, desert dust and high-ultraviolet conditions the coating is consumed and then the steel starts to corrode. Stainless steel profiles remove that maintenance cycle: the passive chromium oxide film reforms when scratched, so a rack that is installed correctly stays serviceable for the life of the modules without coating inspection.
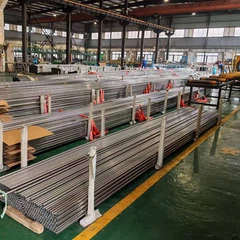
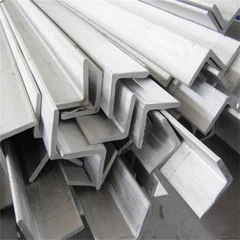
Profiles are supplied as C, U, L, Z and T sections, plus project-specific shapes, and they form the beams, rails, brackets, purlins and clamps of rooftop, ground-mount and tracker systems. Because the profiles are both the structure and the visible finish, dimensional consistency and surface quality matter as much as the grade itself.
Grade Selection: 304, 304L, 316 and 316L
| Grade | Key alloying | Best suited to | Annealed minimums |
|---|---|---|---|
| 304 | 18-20% Cr, 8-10.5% Ni | Inland and desert sites, low chloride exposure | 515 MPa tensile / 205 MPa yield |
| 304L | Lower carbon | Welded assemblies in mild environments | 485 MPa tensile / 170 MPa yield |
| 316 | 16-18% Cr, 10-14% Ni, 2-3% Mo | Coastal and industrial atmospheres | 515 MPa tensile / 205 MPa yield |
| 316L | 316 with lower carbon | Coastal sites, welded joints, high-chloride exposure | 485 MPa tensile / 170 MPa yield |
The listed values are annealed minimums. Roll forming and cold bending raise both tensile and yield strength above these figures, so a formed profile is stronger than the flat strip it was made from; where a design relies on that work-hardened strength, the formed condition and the acceptance test have to be agreed in advance. Molybdenum is the decisive element: 316 and 316L carry 2-3% Mo for chloride resistance, while 304 and 304L rely on chromium alone and are the economical choice where chlorides stay low.
Profile Types and Dimensional Range
| Parameter | Range | Notes |
|---|---|---|
| Profile types | C, U, L, Z, T and custom sections | Beams, rails and brackets |
| Thickness | 1.5 - 6.0 mm | Thickness tolerance about plus or minus 0.05 mm |
| Width / developed width | 30 - 200 mm | Made to drawing |
| Length | 2 - 12 m | Cut to size for the project |
| Surface finish | 2B, BA, brushed or pickled | Pickled and passivated for coastal use |
| Corrosion testing | 1000 h and above, neutral salt spray | ASTM B117 |
Material is produced to ASTM A240, EN 10088-2 or JIS G4304 depending on the market, and is formed by roll forming or press braking with nitrogen-protected processing so the surface does not discolour. Laser cutting gives square, burr-free ends, which keeps module clamps sitting flat and avoids the point loads that distort a rail over time.
Corrosion Performance in Coastal and Desert Conditions
Two mechanisms dominate in the field. The first is chloride attack: sea air deposits salt on the surface, and once the deposit is wet the local chemistry attacks the passive film. 316L is the standard answer, and in splash zones or where salt accumulates, drainage paths and washing access should be designed in so chloride does not concentrate in crevices. The second is abrasion by wind-borne sand, which removes the passive film mechanically. Thicker sections and a pickled or brushed finish help, and edges should be de-burred because a rough edge is where corrosion starts.
Heat and ultraviolet exposure are less damaging to stainless than to coated steel, but they raise demands on the modules and cabling rather than on the profile. Thermal movement over a large array still has to be accommodated, so slotted connections and correctly sized expansion gaps belong in the design regardless of grade. The practical conclusion is that a stainless rack does not need a maintenance budget, but it does need correct grade selection and clean drainage detailing.
Fabrication, Cutting and Installation
Cut and drill with dedicated stainless tooling; carbon-steel brushes or blades contaminate the surface and seed rust spots.
Deburr every cut edge and remove swarf before assembly, since embedded iron particles are the most common cause of early staining.
Use stainless fasteners with the same or a more highly alloyed grade than the profile, and isolate stainless from galvanised steel with a suitable washer or gasket to avoid galvanic effects.
Do not use chlorinated lubricants or cleaning agents on 304 or 316 assemblies.
Pickle and passivate welds on coastal projects, then rinse thoroughly before handover.
Quality Control and Delivery Planning
Each production lot should be traceable to a heat number and supported by a certificate of analysis, dimensional records and salt-spray results where the project requires them. For a large array, the practical risk is not metallurgy but logistics: profiles are long, easily damaged in transit and expensive to reorder, so lengths are usually cut to the module spacing, bundled by structure type and packed to protect the finished surface during shipping. Project schedules are best built around a rolling delivery plan matched to installation sequence rather than a single bulk shipment.
Frequently Asked Questions
Q: Which grade is best for a coastal photovoltaic plant?
316L is the usual choice for maximum chloride resistance, especially at welded joints and in splash zones, while 304 or 304L is economical and sufficient for inland desert sites where salt deposition stays low.
Q: How long do stainless profiles last in a solar array?
With correct grade selection and clean installation, service life extends beyond the module warranty period, and the profiles do not need the periodic recoating that galvanised structures require.
Q: Can profile shapes and dimensions be customised?
Yes. Section shape, thickness, width and length are produced to drawing, and C, U, L, Z and T sections are standard starting points for beams, rails and brackets.
Q: What thickness tolerance can be held?
Roll-formed profiles are typically held to about plus or minus 0.05 mm on thickness within the 1.5 to 6.0 mm range, with cut lengths matched to the module layout.
Q: Does stainless steel reduce maintenance cost on a tracker system?
It removes coating maintenance and repainting, and it avoids the corrosion-driven fastener seizure that complicates tracker repairs, which is where most long-term structural cost occurs.
Q: How are the profiles protected in transit?
Bundles are strapped and packed with surface protection, tagged by heat number and arranged by structure type so that unpacking follows the installation sequence on site.
Send Inquiry