

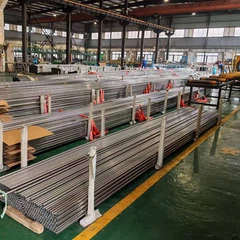
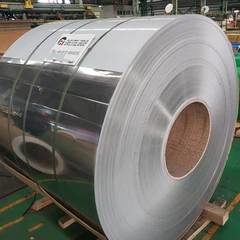
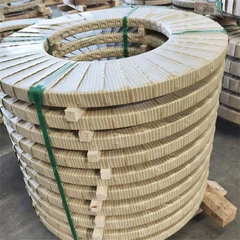
321H Stainless Steel (UNS S32109): High-Carbon Titanium-Stabilized Grade for Elevated-Temperature Service
Dec 11, 2025
Leave a message
321H belongs to the titanium-stabilized austenitic family. The H suffix denotes a controlled carbon range of 0.04-0.10%, which is higher than the 0.08% maximum of standard 321. The extra carbon combines with titanium to form more titanium carbides, and those carbides restrict grain-boundary sliding at elevated temperature, raising creep strength and stress-rupture life. 321H is therefore specified where welded or cold-formed parts must hold load at 800-900°C. Designations: UNS S32109, ASTM A240 Type 321H, ASTM A213 TP321H, JIS SUS321H, legacy DIN X10CrNiTi18-10. Within EN 10088 the closest standard grade is 1.4541 (X6CrNiTi18-10), which covers the base 321 composition.
Chemical Composition per ASTM A240
The limits below apply to plate, sheet and strip per ASTM A240 Type 321H; the tubular form TP321H per ASTM A213 carries the same requirements.
| Element | Content, % |
|---|---|
| Carbon (C) | 0.04-0.10 |
| Manganese (Mn) | 2.00 max |
| Phosphorus (P) | 0.045 max |
| Sulfur (S) | 0.030 max |
| Silicon (Si) | 0.75 max |
| Chromium (Cr) | 17.00-19.00 |
| Nickel (Ni) | 9.00-12.00 |
| Titanium (Ti) | 5×C min, 0.70 max |
Mechanical Properties
In the annealed condition, 321H meets the same minimum room-temperature properties as 321.
| Property (annealed) | Value |
|---|---|
| Tensile strength, MPa | 515 min |
| 0.2% yield strength, MPa | 205 min |
| Elongation (plate, A240), % | 40 min |
| Brinell hardness, HBW | 217 max |
The advantage of 321H appears at temperature: finer and more numerous titanium carbides raise yield strength at 850°C by roughly 15-20% compared with 321, and improve stress-rupture life at 800-900°C, which is the basis for its use in boiler superheater and reheater tubes.
High-Temperature Performance
321H is applied for continuous service up to about 900°C in oxidizing and mildly corrosive atmospheres, sitting between 321 at about 870°C and 309S at about 980°C. Design codes treat the H designation differently from the base grade: pressure-vessel rules permit 321H at higher temperatures than 321 because its creep data are documented and its carbides remain stable. At 850°C, 321H shows substantially less creep deformation than 321 over the same stress and time, which is why superheater tubing in this range is routinely specified as TP321H. Titanium stabilization also preserves intergranular corrosion resistance after welding, because the titanium content is scaled to carbon at 5×C minimum, so no chromium-depleted zones form at grain boundaries.
Fabrication and Welding
321H welds by the same processes as 321, but the higher carbon content demands discipline. Use matching stabilized filler, such as a titanium-bearing filler for 321H, because an unstabilized filler reintroduces the sensitization risk; keep heat input low and interpass temperature below about 150°C; and clean joint surfaces thoroughly because titanium is easily oxidized and lost from the weld pool. Bending requires more force than 321 because of the higher yield strength, and heavily cold-formed parts should be solution annealed before high-temperature service. Machining proceeds about 10-15% slower than 321 due to the higher hardness, and carbide tooling is recommended. Post-fabrication annealing at about 950-1120°C followed by rapid cooling restores full ductility and creep performance.
Applications and Selection
Typical 321H components are boiler superheater and reheater tubes, steam piping, turbine internals, heavy-duty furnace elements, expansion bellows, and any welded part that carries stress at 800-900°C. Selection guidance: use standard 321 below about 870°C where stresses are low and cost matters; use 321H where the part must hold load at 800-900°C; and consider 347H where even higher creep strength and niobium carbide stability are required, or 309S/310S where scaling resistance above 900-1000°C dominates. In sulfur-rich combustion atmospheres, the titanium-stabilized grades are generally preferred over niobium-stabilized grades because niobium can form brittle sulfides.
Frequently Asked Questions
Q1: Why does higher carbon improve 321H at high temperature? A1: The 0.04-0.10% carbon reacts with titanium to form more titanium carbides than in 321. These fine carbides pin grain boundaries and slow the atomic diffusion that drives creep, raising yield strength at 850°C by roughly 15-20% and extending stress-rupture life.
Q2: Does 321H keep the corrosion resistance of 321? A2: Yes. Titanium is specified at 5×C minimum, so for 0.10% carbon the minimum titanium is 0.50%, which binds essentially all carbon and prevents chromium-depleted zones. Intergranular corrosion resistance after welding matches 321.
Q3: What is the maximum service temperature of 321H? A3: Continuous service is generally limited to about 900°C in oxidizing atmospheres. Between 870°C and 900°C, 321H is preferred over 321 for load-bearing parts; above 900°C consider 309S, 310S or 347H depending on stress and atmosphere.
Q4: How is 321H welded? A4: By GTAW, GMAW or SMAW with titanium-bearing stabilized filler, low heat input, interpass temperature below about 150°C, and clean joint faces. Post-weld heat treatment is not required for corrosion resistance.
Q5: What is the EN equivalent of 321H? A5: EN 10088 does not define an H-grade; the closest EN 10088 grade is 1.4541 (X6CrNiTi18-10), which matches standard 321. The H designation exists in ASTM A240, ASTM A213, ASME SA-240 and SA-213, and in JIS as SUS321H.
Q6: When should I choose 321H instead of 347H? A6: Choose 321H for 800-900°C load-bearing service where cost matters and welding is straightforward; 321H is typically cheaper than 347H. Choose 347H where maximum creep strength and niobium carbide stability justify the higher price, and note that 321H is usually preferred in sulfur-rich atmospheres.
Send Inquiry